 01
Design
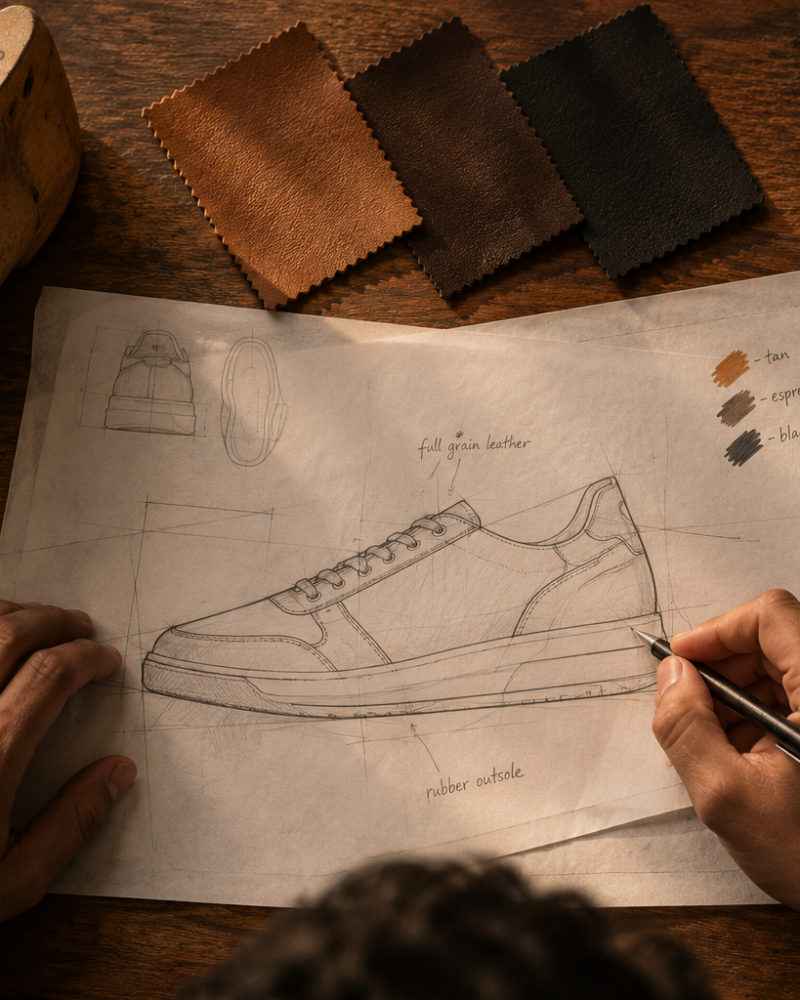
Concepts are drawn in-house, then reviewed against the buyer’s market, price point and season.
Capabilities
Design, development, manufacturing and quality control under one roof in Agra.
Design & development
Development happens in-house. 33+ original designs have been taken from concept through to a sample a buyer can hold, and the same route is open to a brand arriving with its own idea.
A brief, a market and a price point become a drawn idea.
Leather, textile, PU and components are matched to the design.
Last, pattern and sole are worked out together, not in sequence.
A first physical version to test the shape and the fit.
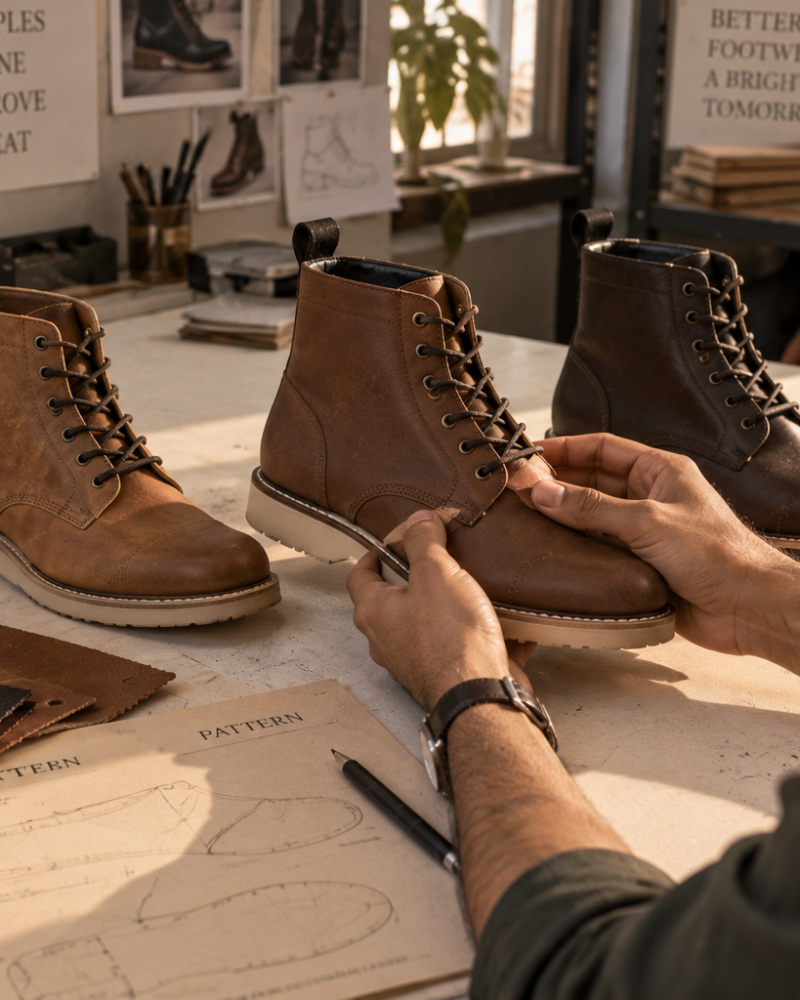
A buyer-ready pair, made the way production would make it.
Changes to material, colour, fit or detail until it is signed off.
The approved sample becomes the standard the line works to.
Manufacturing
01
Concepts are drawn in-house, then reviewed against the buyer’s market, price point and season.
 02
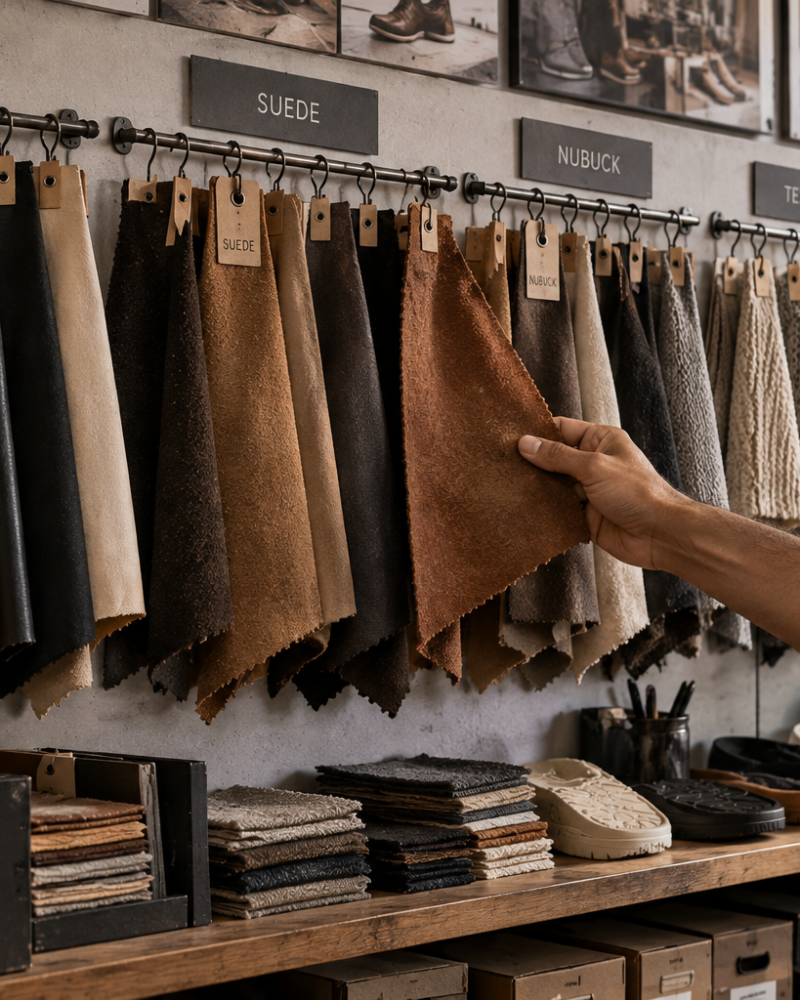
Leather, suede, textile, PU and components are selected and matched to the construction.
 03
A buyer-ready sample is produced, assessed and refined until the specification is signed off.
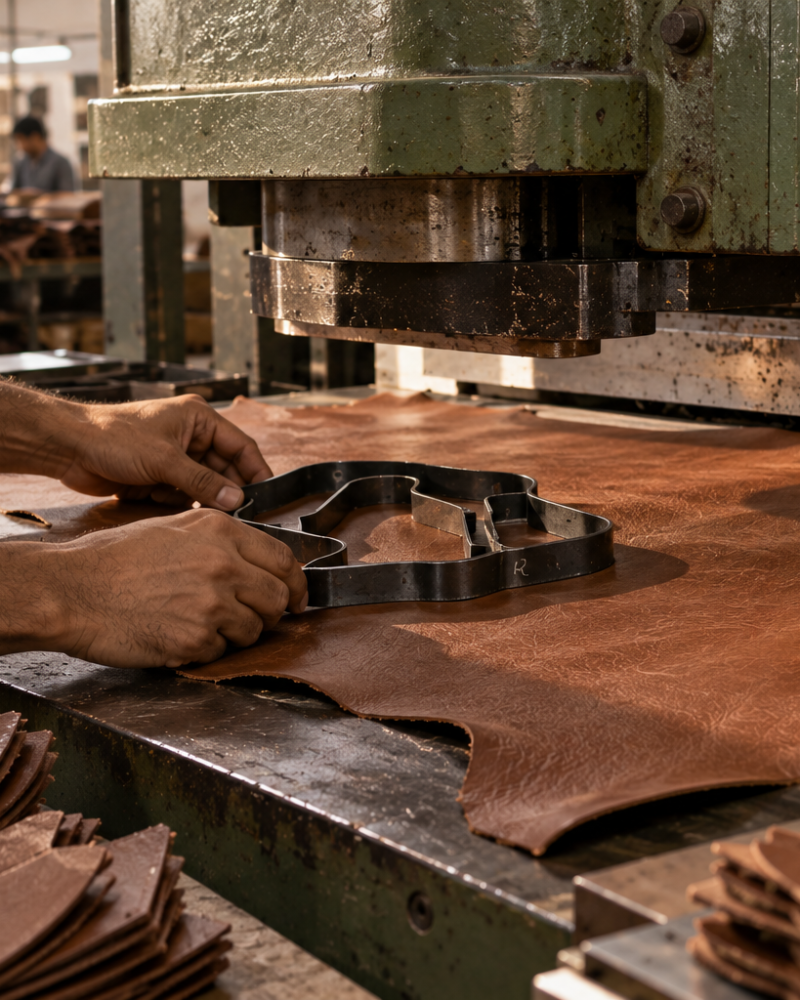 04
Panels are cut to the approved pattern, with material inspected before it enters the line.
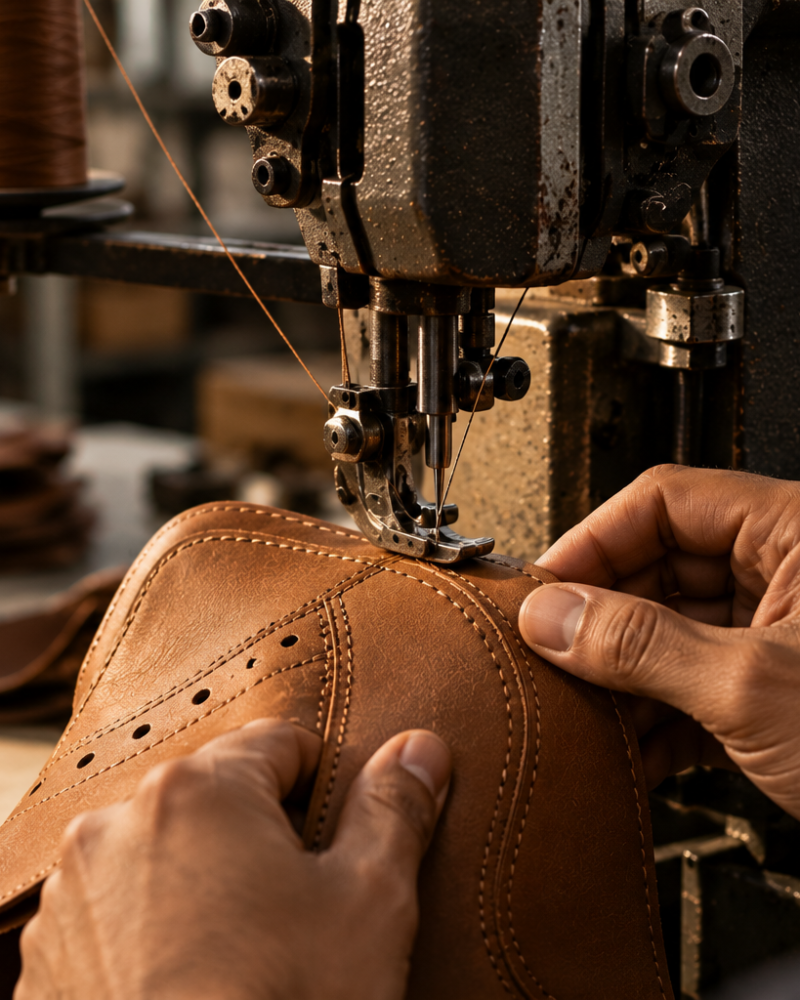 05
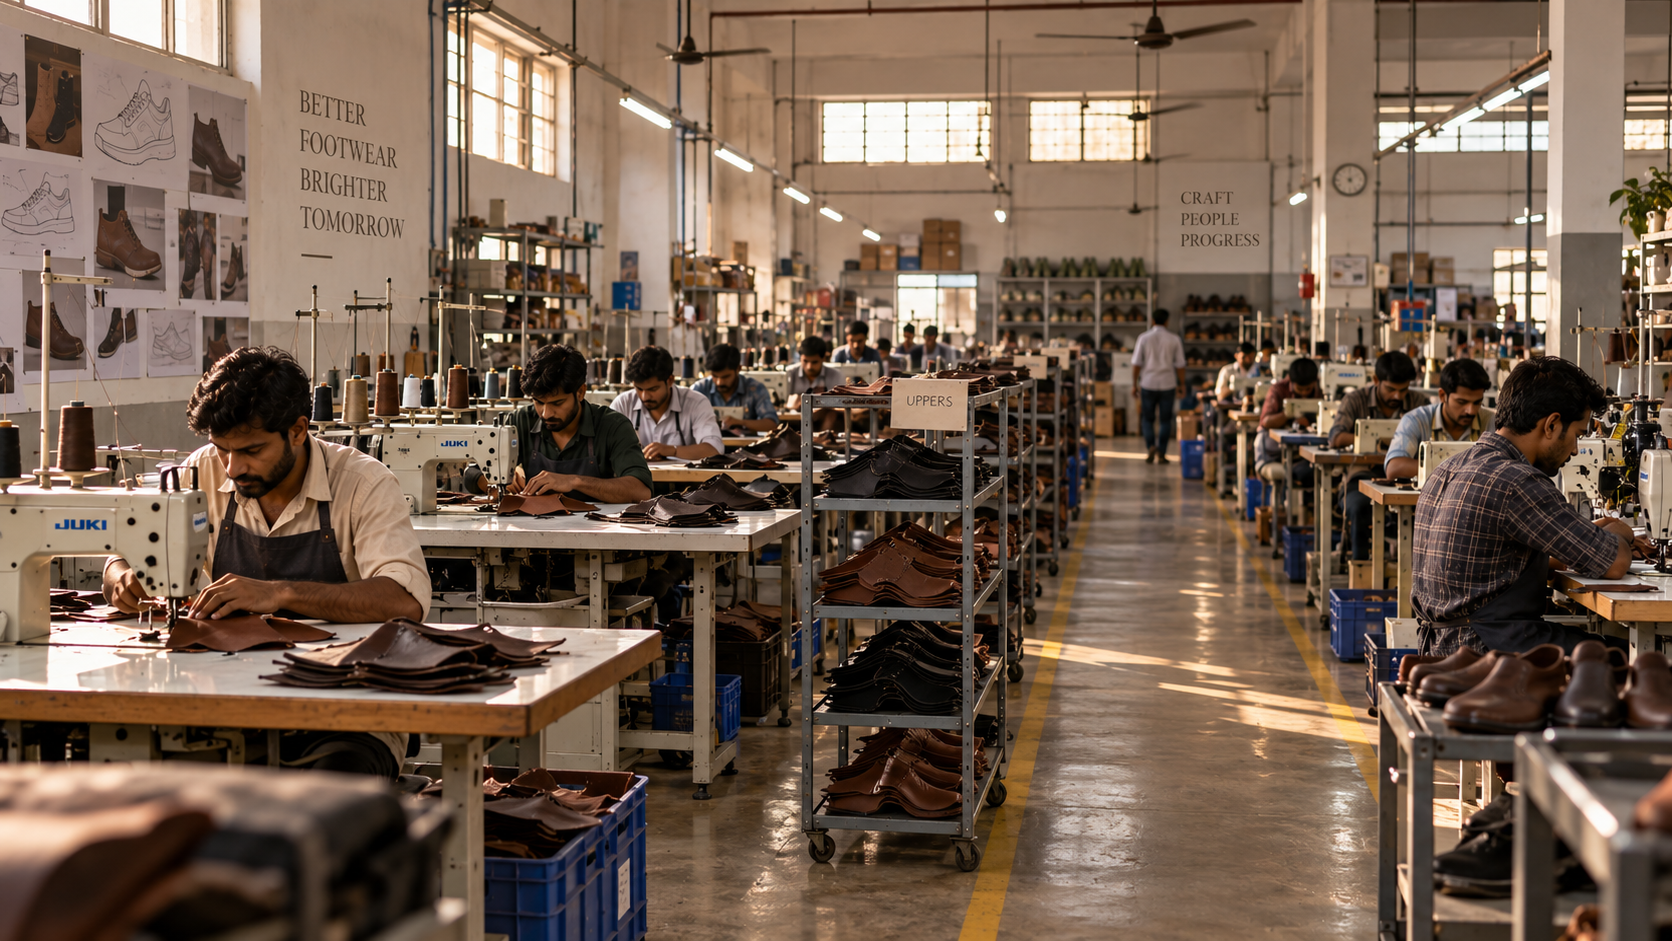
Uppers are closed by trained operators working to the approved sample.
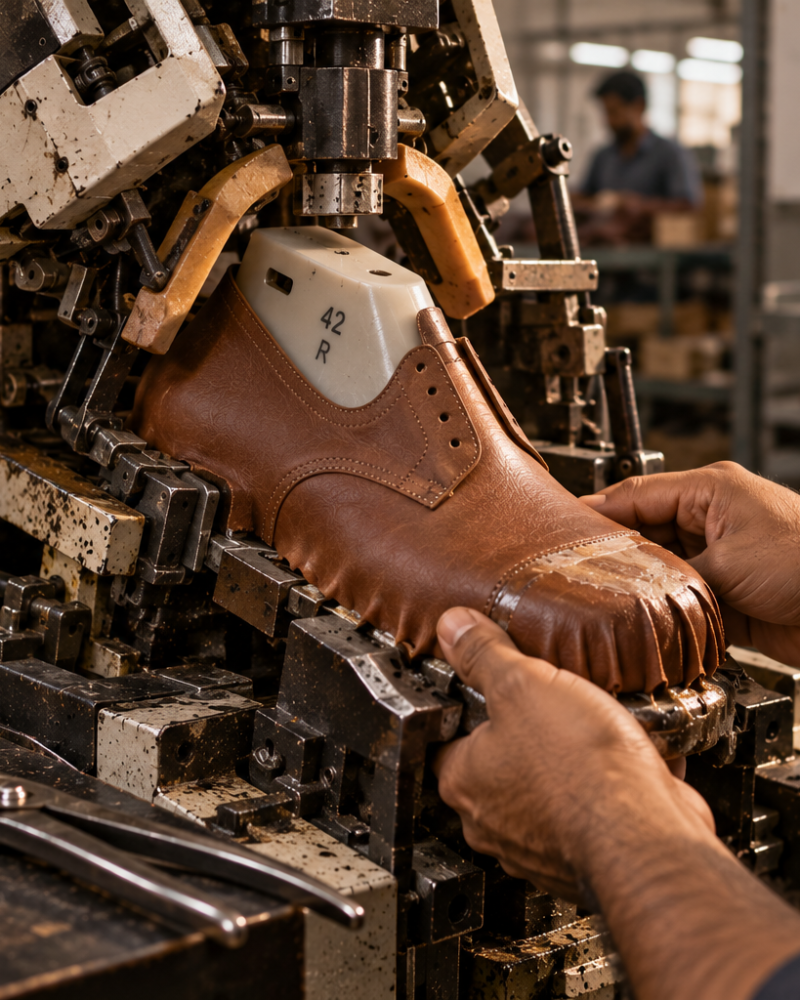 06
Uppers are lasted and soles attached to the confirmed construction.
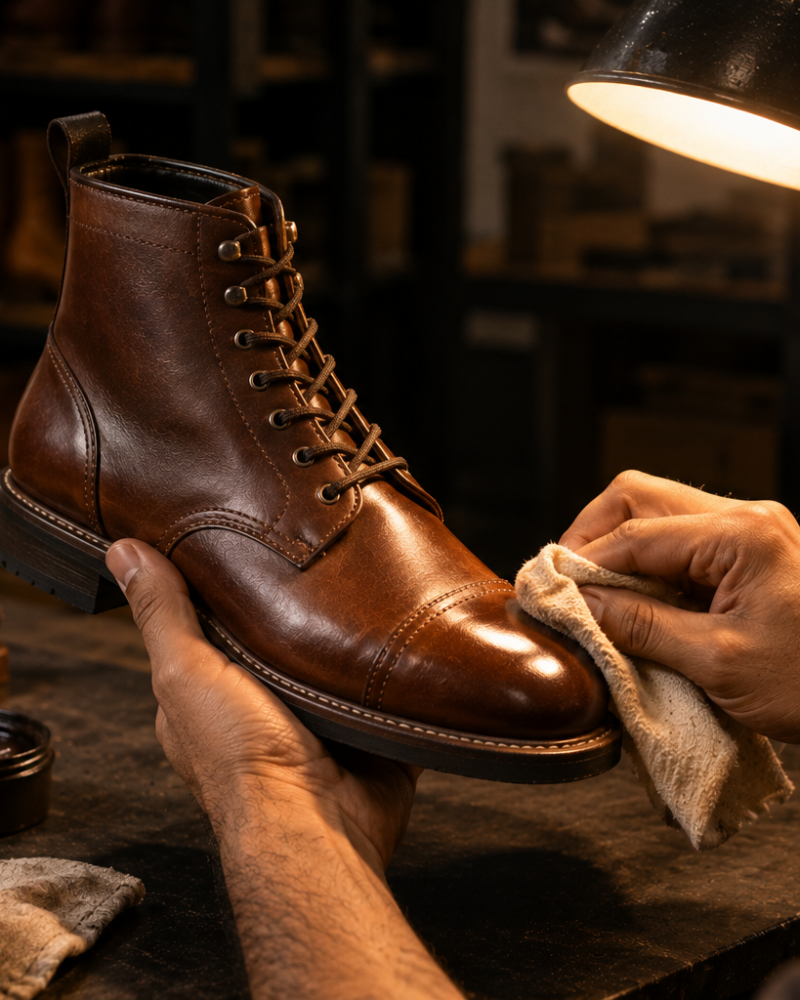 07
Cleaning, conditioning, lacing and final presentation of the pair.
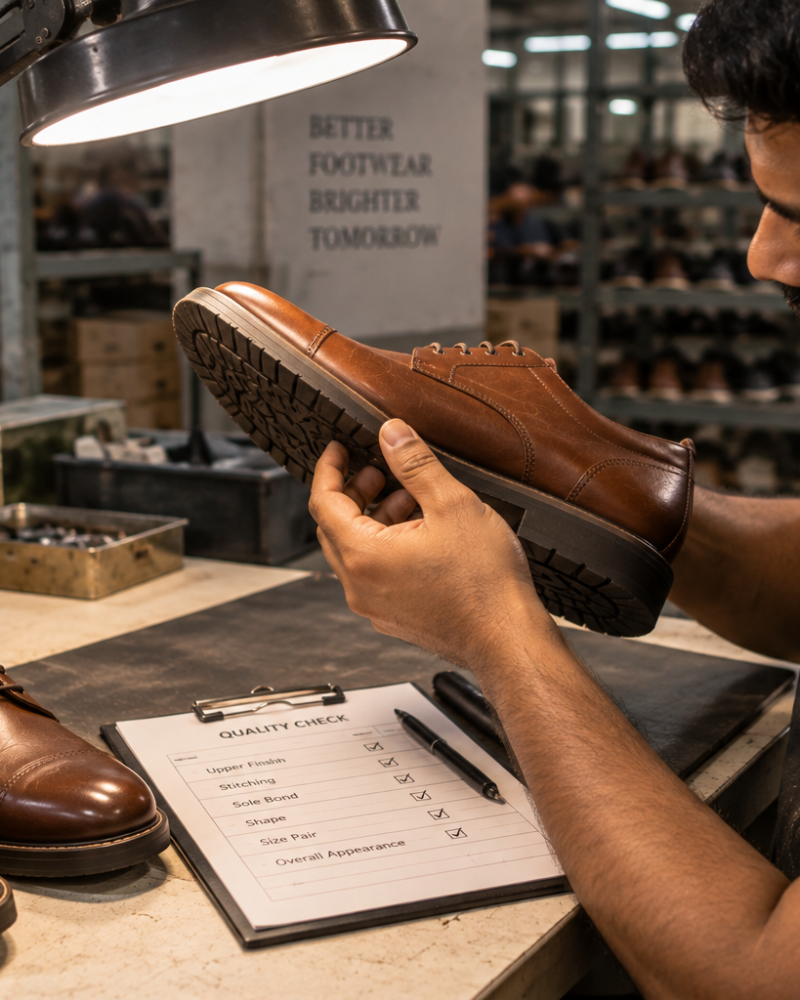 08
Inspection at each stage, and again on the finished pair before packing.
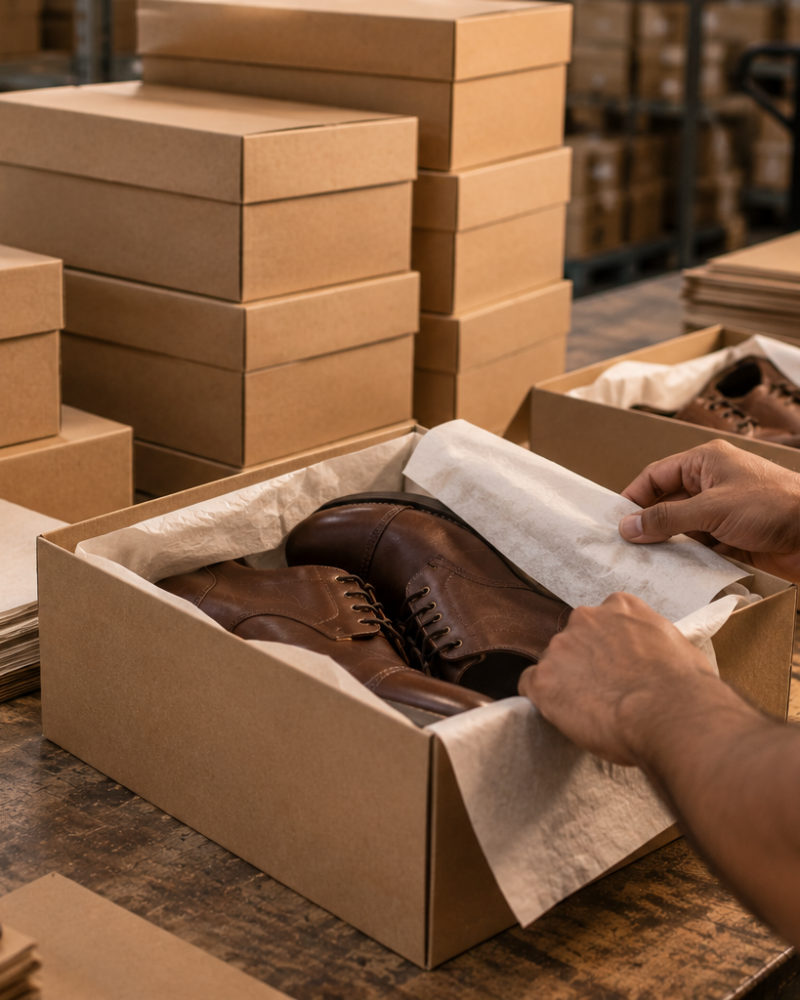 09
Cartons, labelling and packing built to the buyer’s specification.
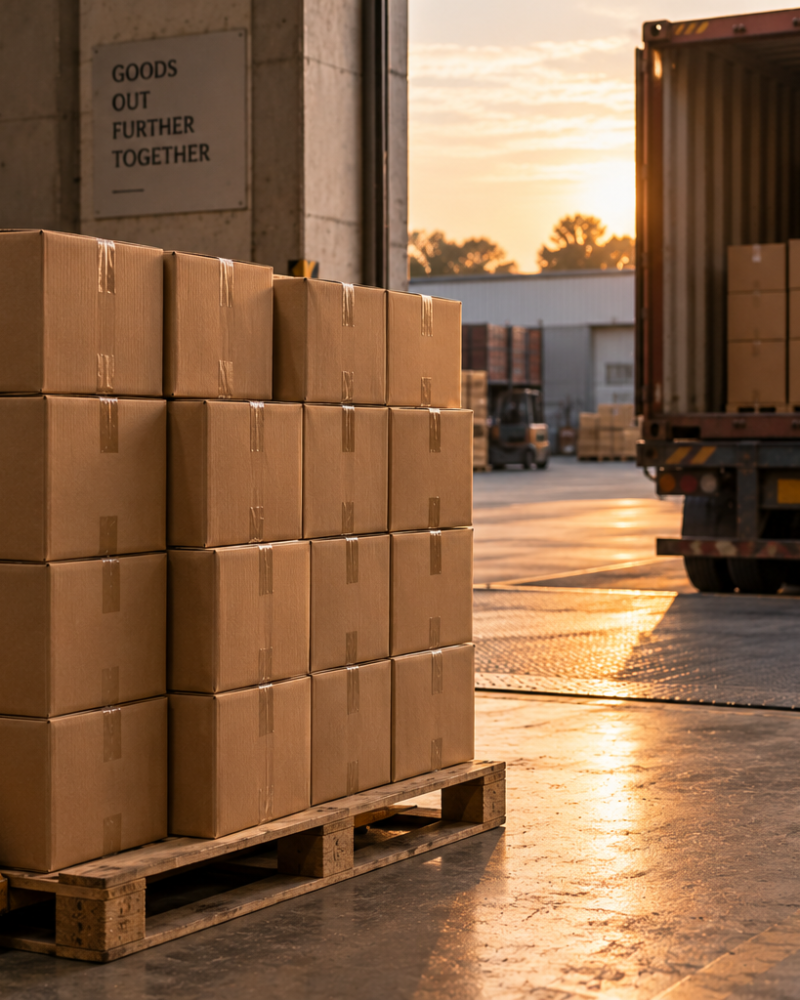 10
Goods are documented, loaded and dispatched to the destination market.
Scroll the line to follow a pair from cutting through to dispatch.
Materials
Upper, lining, sole and components are selected against the construction, the target landed cost and the market a pair is going to. Leather, suede, nubuck, textile and PU uppers are combined with EVA, TPR, PU and rubber soling depending on the weight, flex and wear the style needs. Sourcing is arranged per programme rather than held as fixed stock.
Quality
Inspection sits inside production rather than at the end of it. Material is checked before it is cut, and the pair is assessed again at each stage it passes through, because a fault found at closing costs a component and a fault found at final inspection costs a finished pair.
The reference for every check is the buyer-approved sample. Inspection records can be shared on request, and where a customer runs its own or a third-party inspection programme, we work alongside it.
Scale
Two manufacturing units in Agra, Uttar Pradesh, India.
Enquiry
Product category, destination market and target quantity are enough to begin. We will come back on construction, material options and what development and production would involve — and we will ask before quoting rather than guess.